Xiagang Industrial Park, Jiangyin City, Jiangsu Province, China
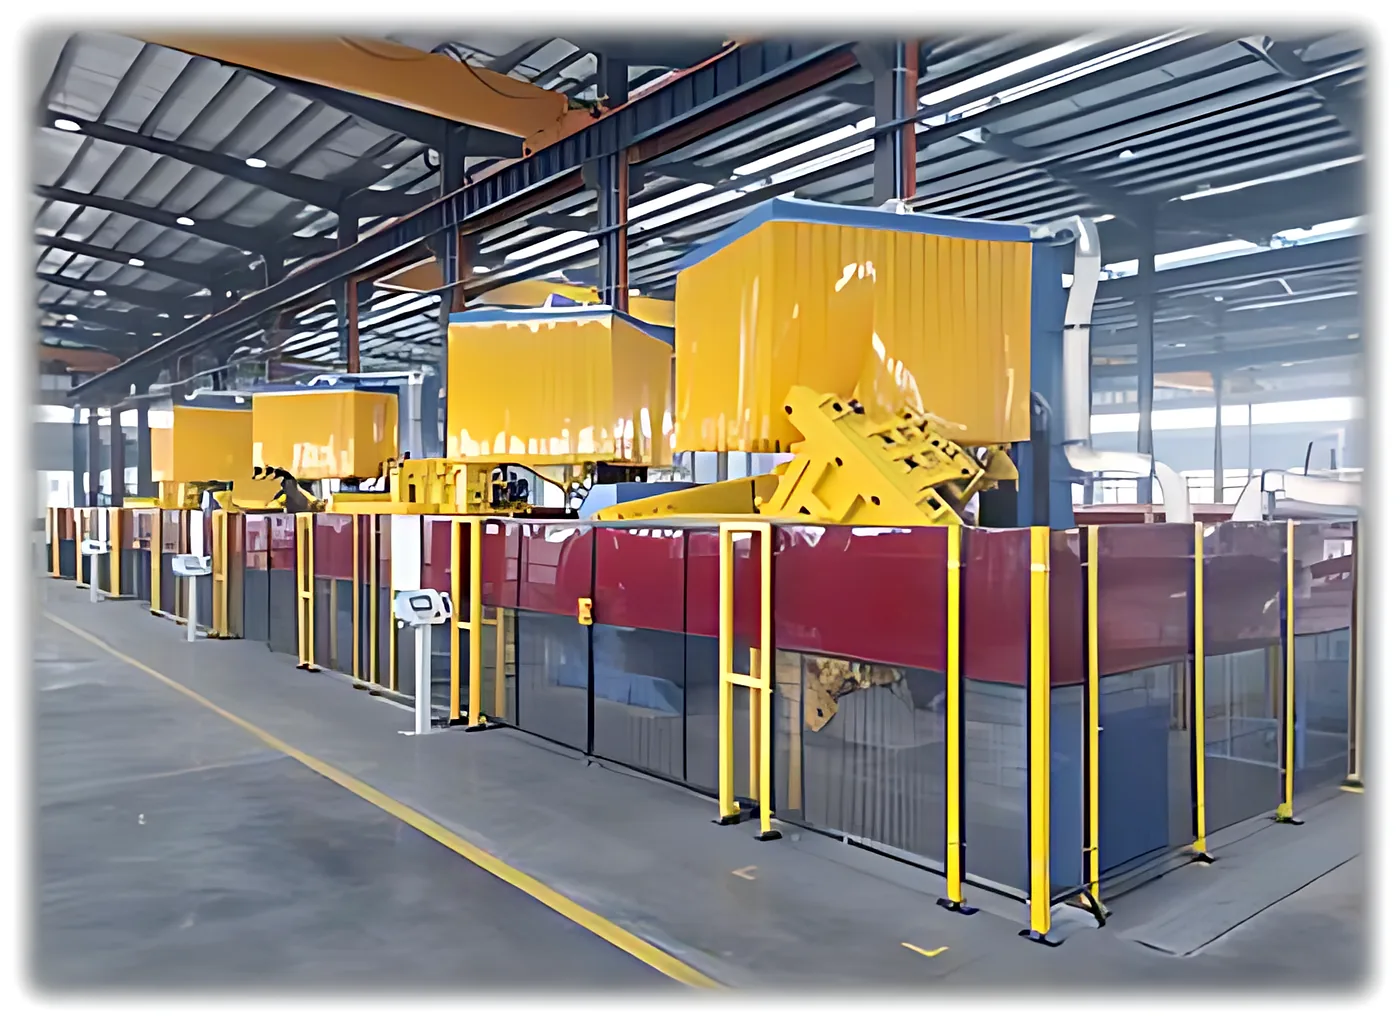
Fabrication shop with robotic welding cells at Songyan Machinery
  1. Home
  2. Capabilities

Machining & Fabrication Capabilities

Turning, milling, grinding, cutting, welding and fabrication, supported by in-house heat treatment, gear cutting, coating and inspection. One production plan takes your part from raw material to a finished, documented component.

6Core processes
1–30,000 kgPart weight
0.01 mmPositioning accuracy
50 tTable load

One process route

Every operation under one roof

A typical welded and machined component passes through up to ten operations. Because all of them run in our own workshops, weld preparation, machining allowances and inspection points are planned together, and your part never waits in transit between subcontractors.

  1. MaterialCertified plate, bar, forgings or castings, verified by spectrometer.
  2. CuttingLaser, plasma or flame cutting with weld bevels prepared.
  3. FormingBending on a 400 t press brake and plate rolling.
  4. WeldingRobotic, submerged arc, TIG and MIG welding to WPS.
  5. Stress reliefThermal or vibratory stress relief before machining.
  6. MachiningBoring, milling and turning to datum on CNC centers.
  7. Heat treatmentQ&T, normalizing, carburizing or induction hardening.
  8. GrindingFinish grinding of journals, faces and gear teeth.
  9. InspectionCMM, NDT and material testing to your control plan.
  10. Coating & packingBlasting, painting, rust protection and export crating.
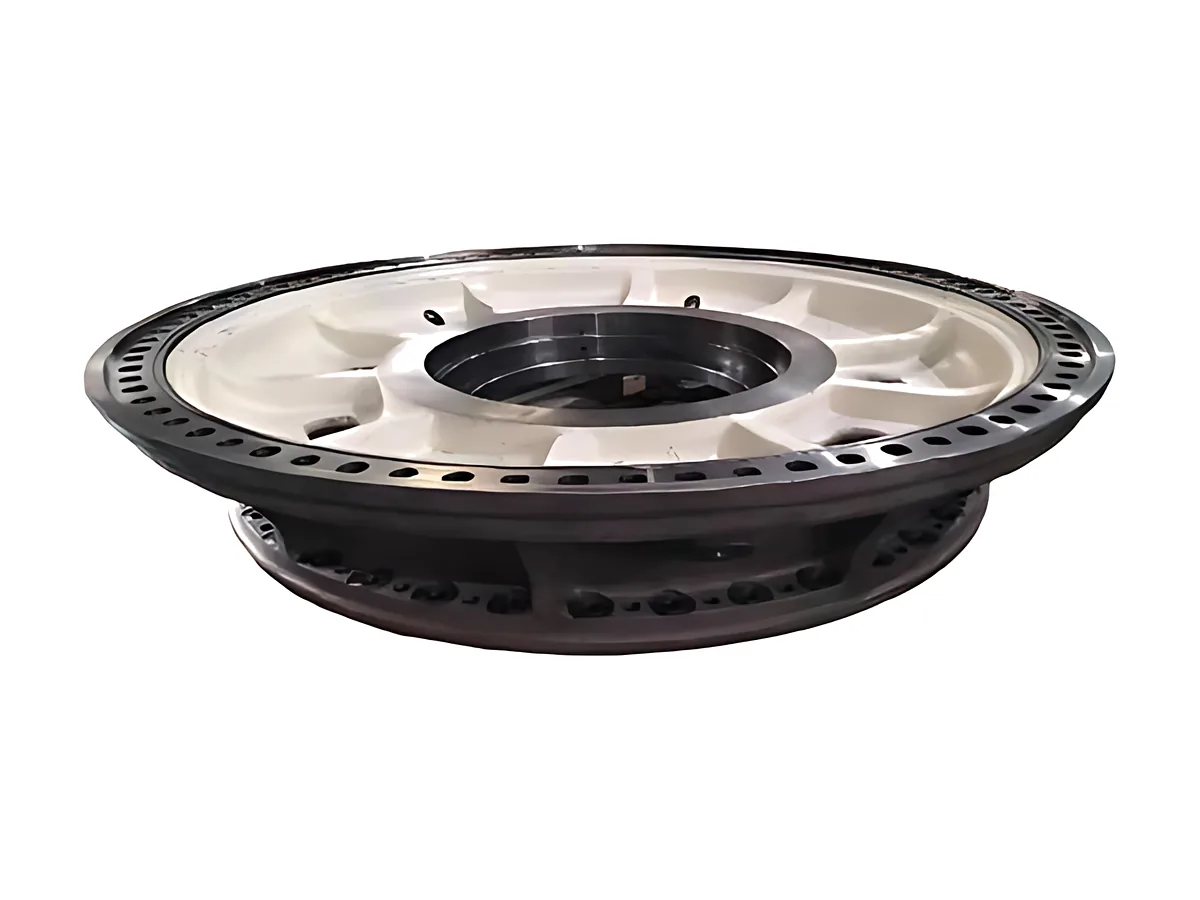
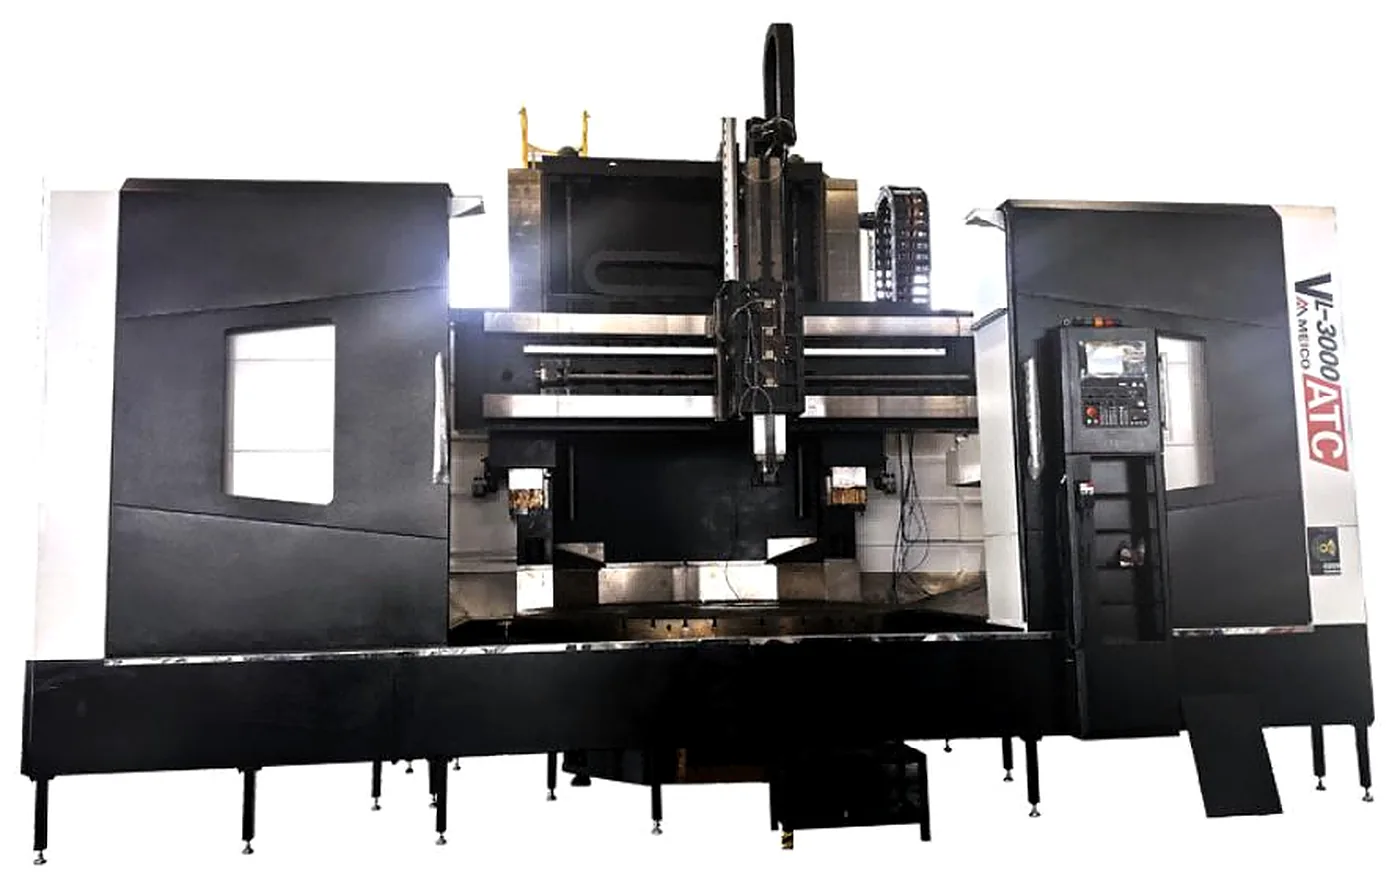
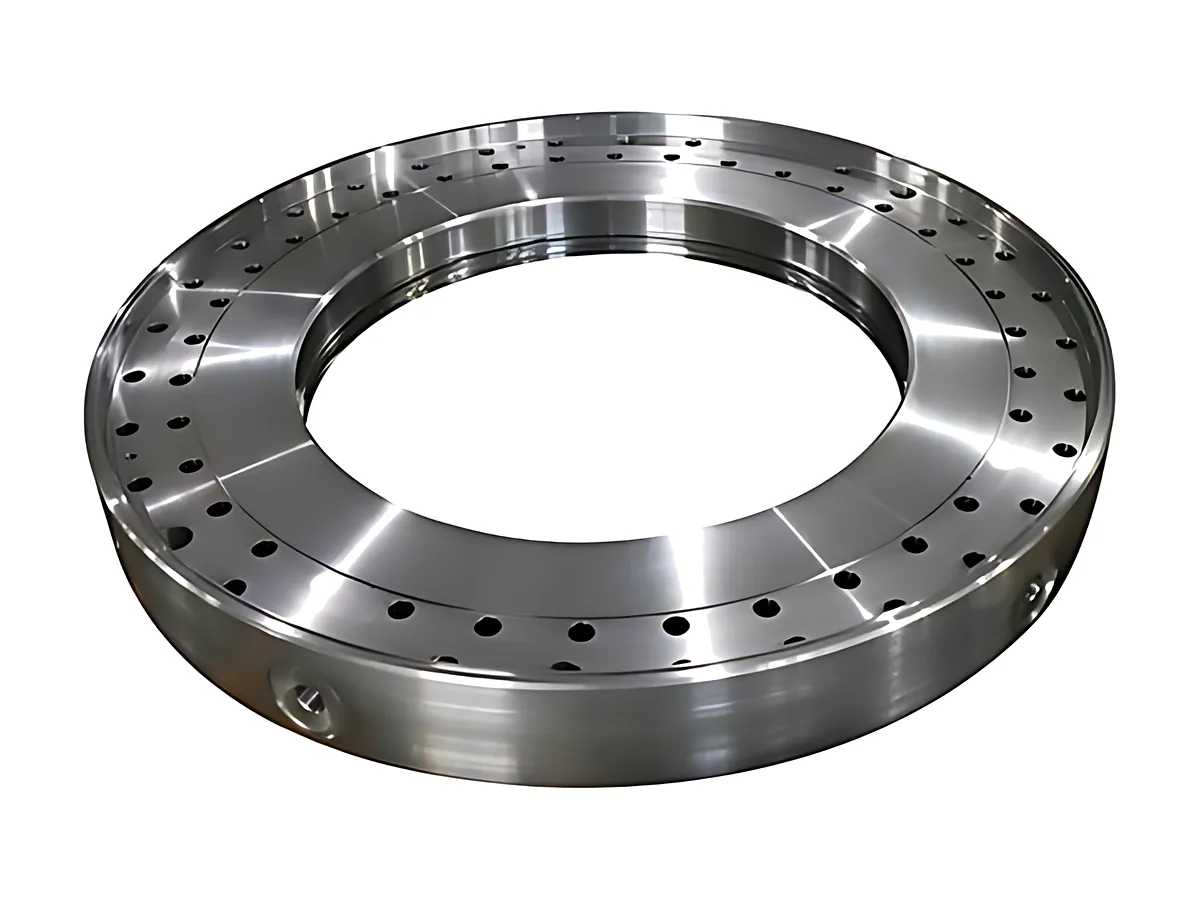
CNC vertical turn-mill center for large rings, discs and housings Large CNC-turned connection flange with drilled bolt circle Process 01 · Turning

Process 01

CNC Turning & Turn-Milling

Shafts, flanges, rings, hubs, sleeves, discs and bowls are turned on horizontal CNC lathes and vertical turning centers. Turn-mill centers with a C-axis and automatic tool changer also mill flats, drill bolt circles and cut keyways in the same clamping, eliminating re-fixturing errors on large rotating parts.

Long shafts are turned between centers with steady rests and finish-ground wherever bearing journals require it.

Vertical turning
Up to the Ø3,200 mm class, 2,000 mm height, 15 t table load
Turn-milling
C-axis indexing to 0.001°, live milling and drilling, ATC
Horizontal turning
Heavy-duty CNC lathes for shafts, rolls and spindles
Typical finish
Ra 1.6–3.2 µm as turned; Ra 0.4–0.8 µm after grinding
Typical parts
Main shafts, flanges, slewing rings, hubs, bowls, sleeves
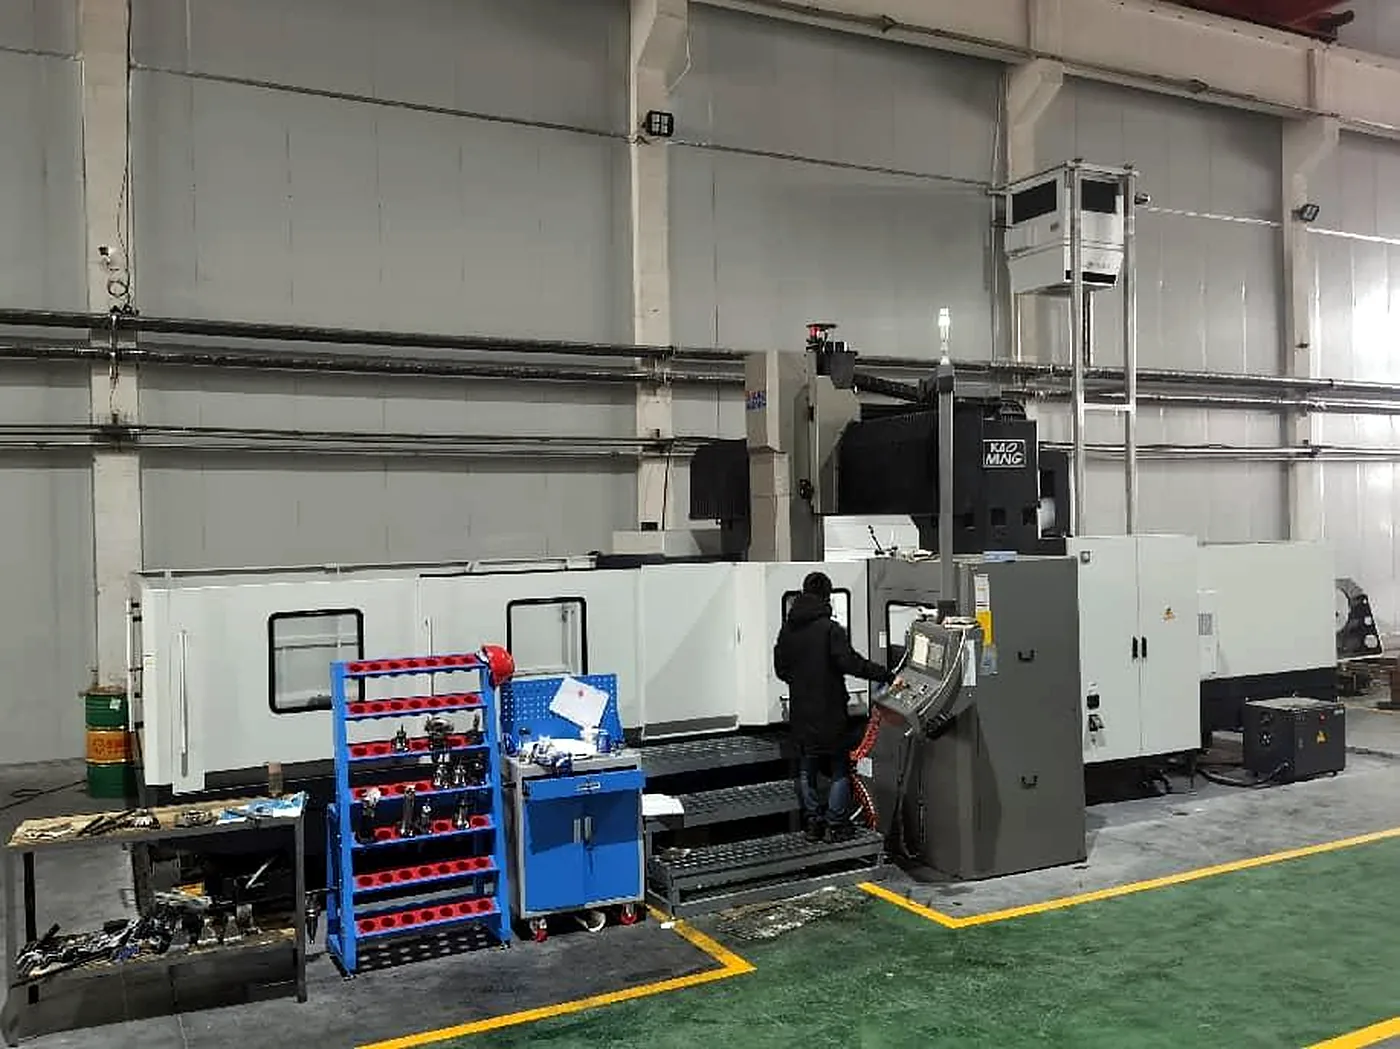
Large horizontal boring and milling center with 50-tonne table CNC-milled and bored wind turbine gearbox housing Process 02 · Milling

Process 02

CNC Milling, Boring & 5-Axis

Gearbox housings, machine beds, frames, valve bodies and brackets are machined on horizontal boring and milling centers, gantry machining centers and 5-axis gantries. Rotary tables allow four faces to be machined in a single setup, keeping bearing bores coaxial and faces square.

For long components, 4-metre planer-type gantry mills machine beds and slideways in one continuous pass.

Horizontal boring
X 5,000 × Y 3,200 × Z 2,500 mm, table load up to 50 t
Gantry machining
X 4,230 × Y 2,650 mm class, plus 5-axis gantry centers
Positioning accuracy
0.01 mm; 0.008 mm on precision horizontal centers
Operations
Line boring, face milling, drilling, tapping, contouring, 5-axis surfaces
Typical parts
Gearbox housings, torque arms, planet carriers, machine bases, BOP bodies
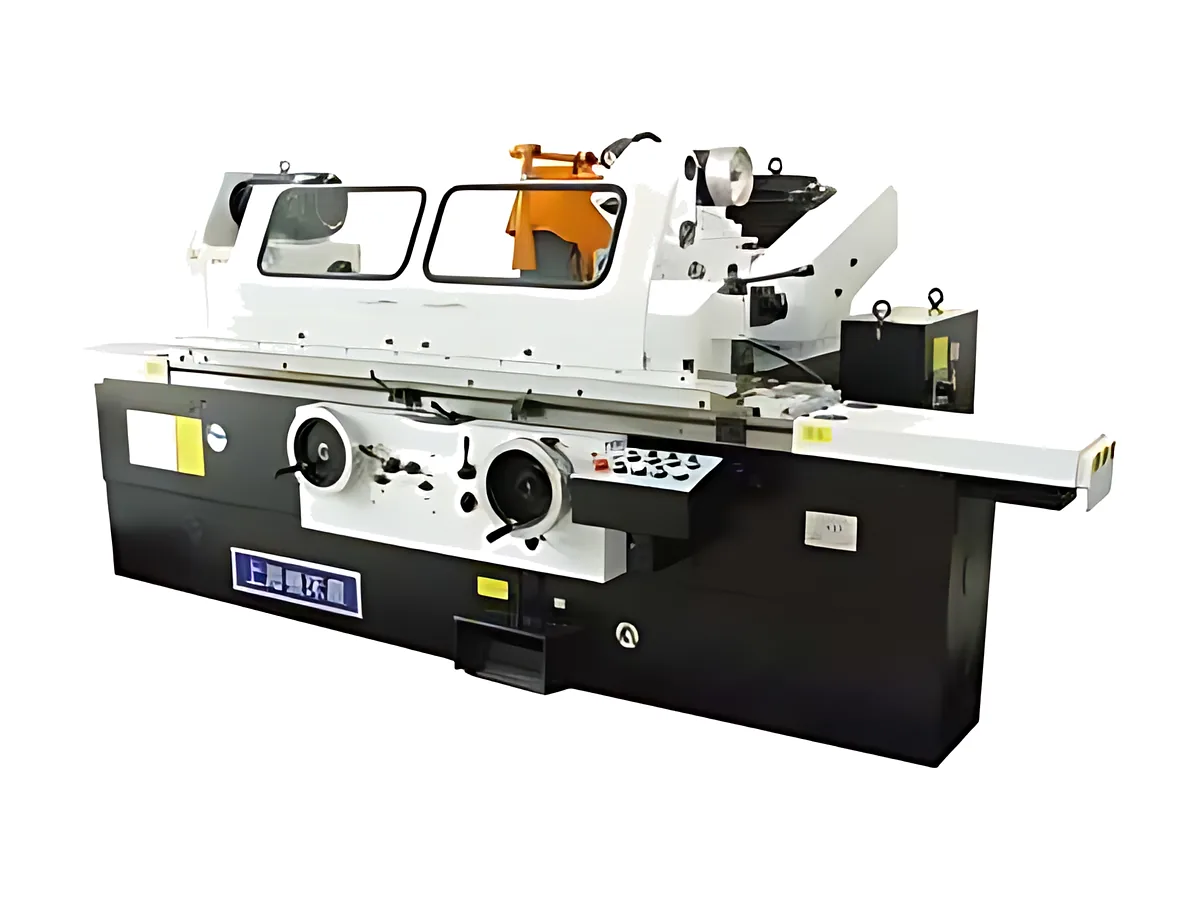
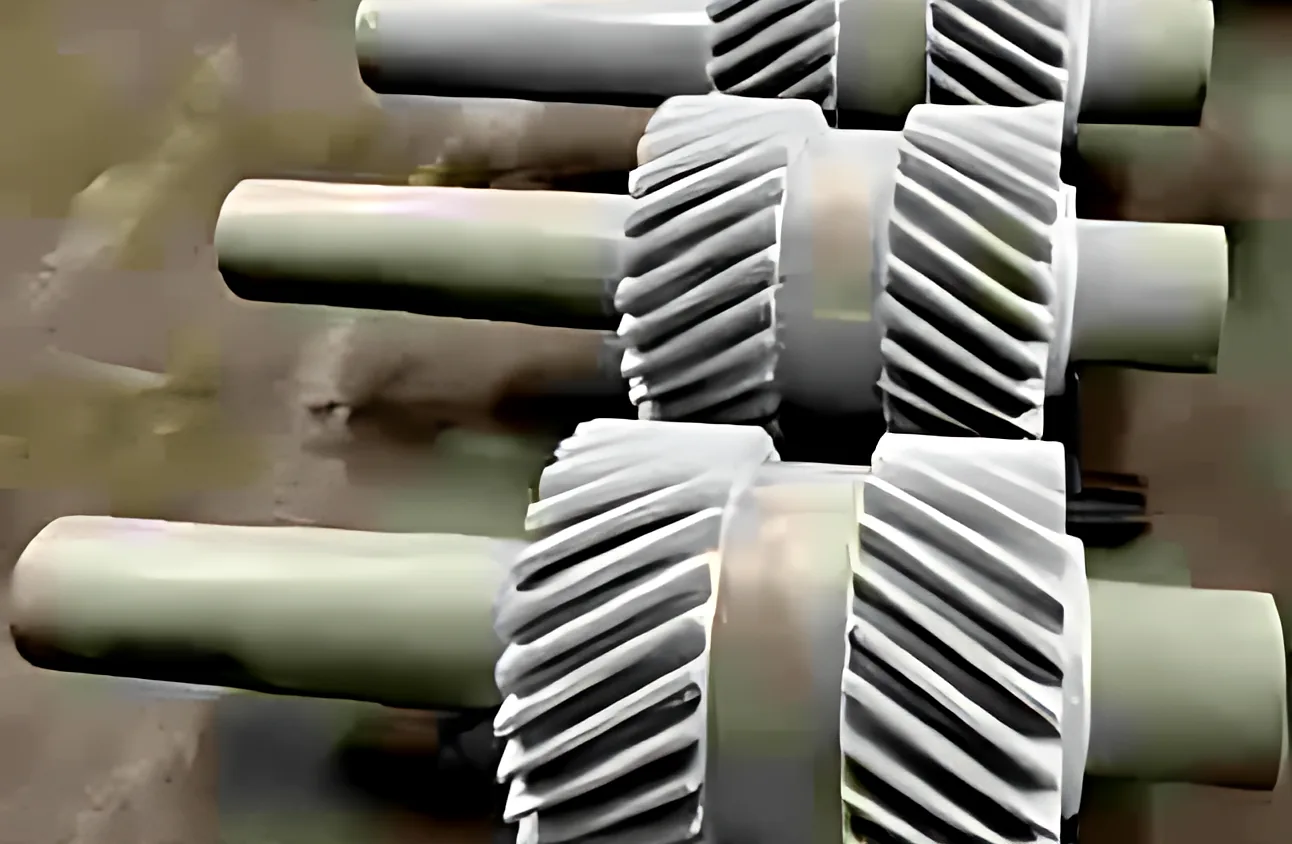
Precision CNC cylindrical grinding machine Ground double-helical gear shafts Process 03 · Grinding

Process 03

Precision Grinding

Cylindrical, surface and gear grinding finish the features that determine service life: bearing journals, seal diameters, mating faces and hardened gear teeth. Grinding follows heat treatment, removing quench distortion and holding final size on the hardened surface.

Cylindrical grinding
Up to Ø630 × 4,000 mm; also Ø500 × 3,000 mm and Ø320 × 1,500 mm machines
Surface grinding
Mounting faces, slideways, wear plates
Gear grinding
Spur and helical teeth after carburizing or induction hardening
Typical finish
Ra 0.4–0.8 µm; IT5–IT6 diameters on suitable geometry
20 kW fiber laser plate cutting machine 12 kW fiber laser tube cutting machine Process 04 · Cutting

Process 04

Laser, Plasma & Flame Cutting

Plate, tube, bar and structural sections are cut from nested programs generated directly from your DXF or 3D model. High-power fiber lasers deliver clean, narrow kerfs on thin and medium plate, while plasma and oxy-fuel handle heavy sections. Weld bevels are cut at this stage for accurate fit-up before the first tack.

Fiber laser, plate
20 kW large-format cutting bed
Fiber laser, tube
12 kW tube and profile cutting
Heavy plate
Plasma and oxy-fuel cutting with bevel preparation
Bar and section
Band-saw cutting of round, square and structural sections
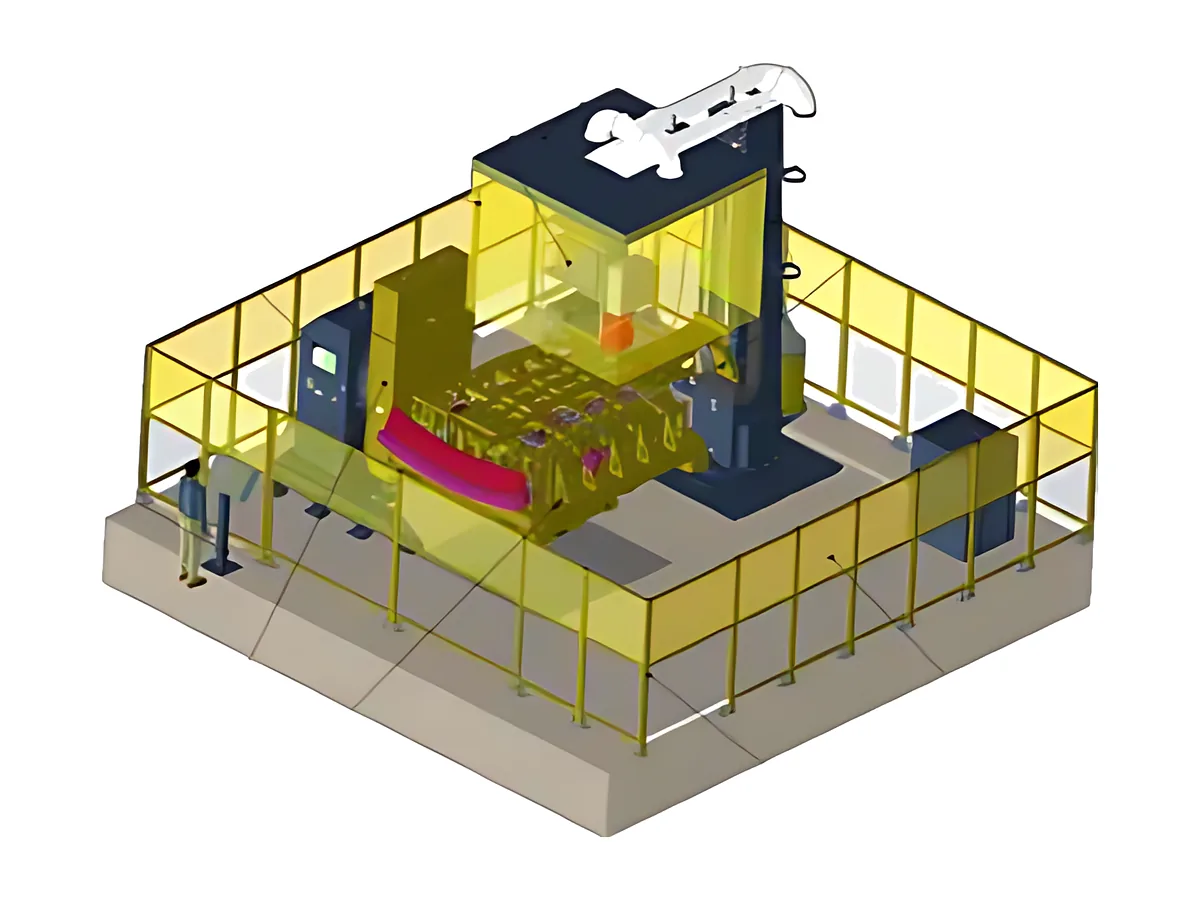
Robotic welding positioners for heavy fabricated frames 10-axis robotic welding system with 6-tonne positioner Process 05 · Welding

Process 05

Robotic & Manual Welding

Long, repeatable seams run on robotic cells with heavy-duty positioners; thick-section joints are filled by submerged arc; root passes and stainless work are carried out by TIG. We weld to your symbols, WPS and NDT requirements, and full-penetration joints are verified by UT or MT before machining.

Robotic welding
10-axis system, 360° positioner, Ø3,650 mm, 6 t capacity
Processes
Pulsed MIG/MAG (550 A), TIG (400 A), submerged arc (1,250 A)
Materials
Carbon, low-alloy, stainless and duplex steels
Weld inspection
Visual, MT and UT; HAZ hardness checks where specified
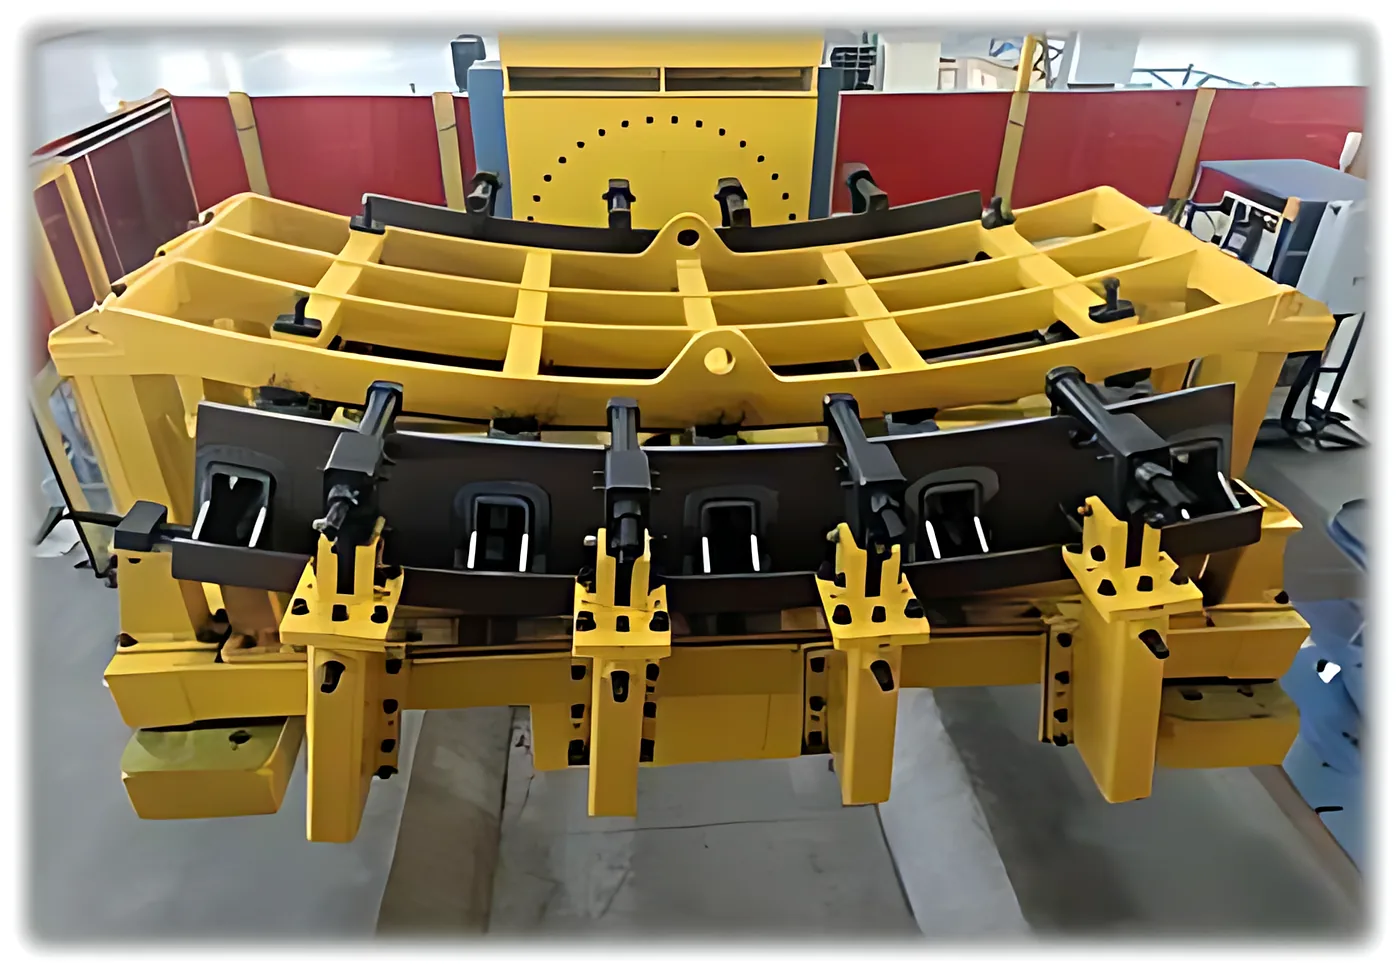
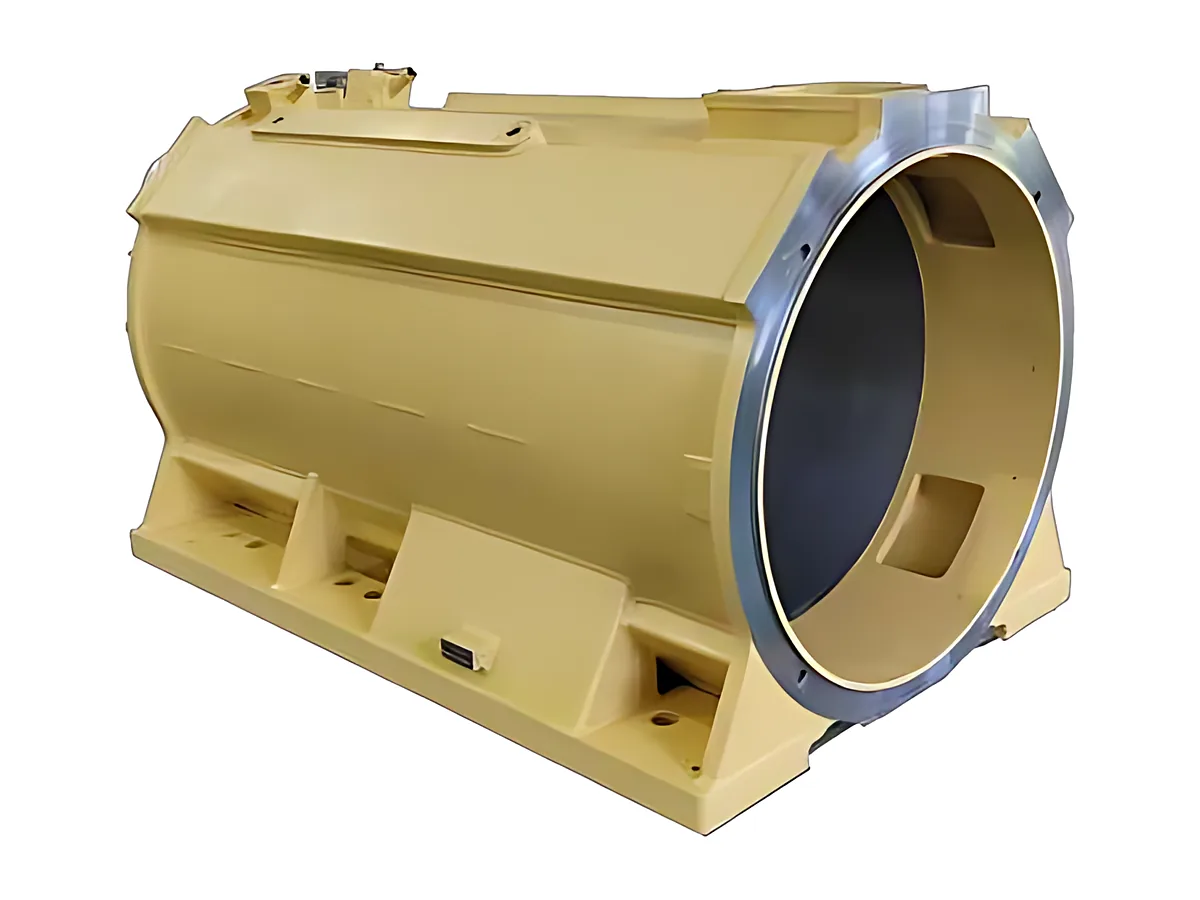
Fabrication shop with robotic welding cells and fixtures Welded, machined and painted generator housing Process 06 · Fabrication

Process 06

Welding & Fabrication

Weldments leave our works as finished components: cut, formed, welded, stress-relieved, machined to datum, blasted and painted. Stress relief is performed thermally in a trolley tempering furnace or by vibratory stress relief before final machining, so bores and faces stay exactly where the drawing places them.

Modular fixtures hold assemblies square during welding and are retained for repeat orders.

Forming
CNC press brake, 400 t × 3,200 mm
Stress relief
Trolley tempering furnace; vibratory stress relief
Post-weld machining
On boring and gantry centers with up to 50 t table load
Finishing
Shot blasting, automatic coating line, paint booths
Typical parts
Machine bases, motor and generator housings, skids, frames, welded rotor shafts
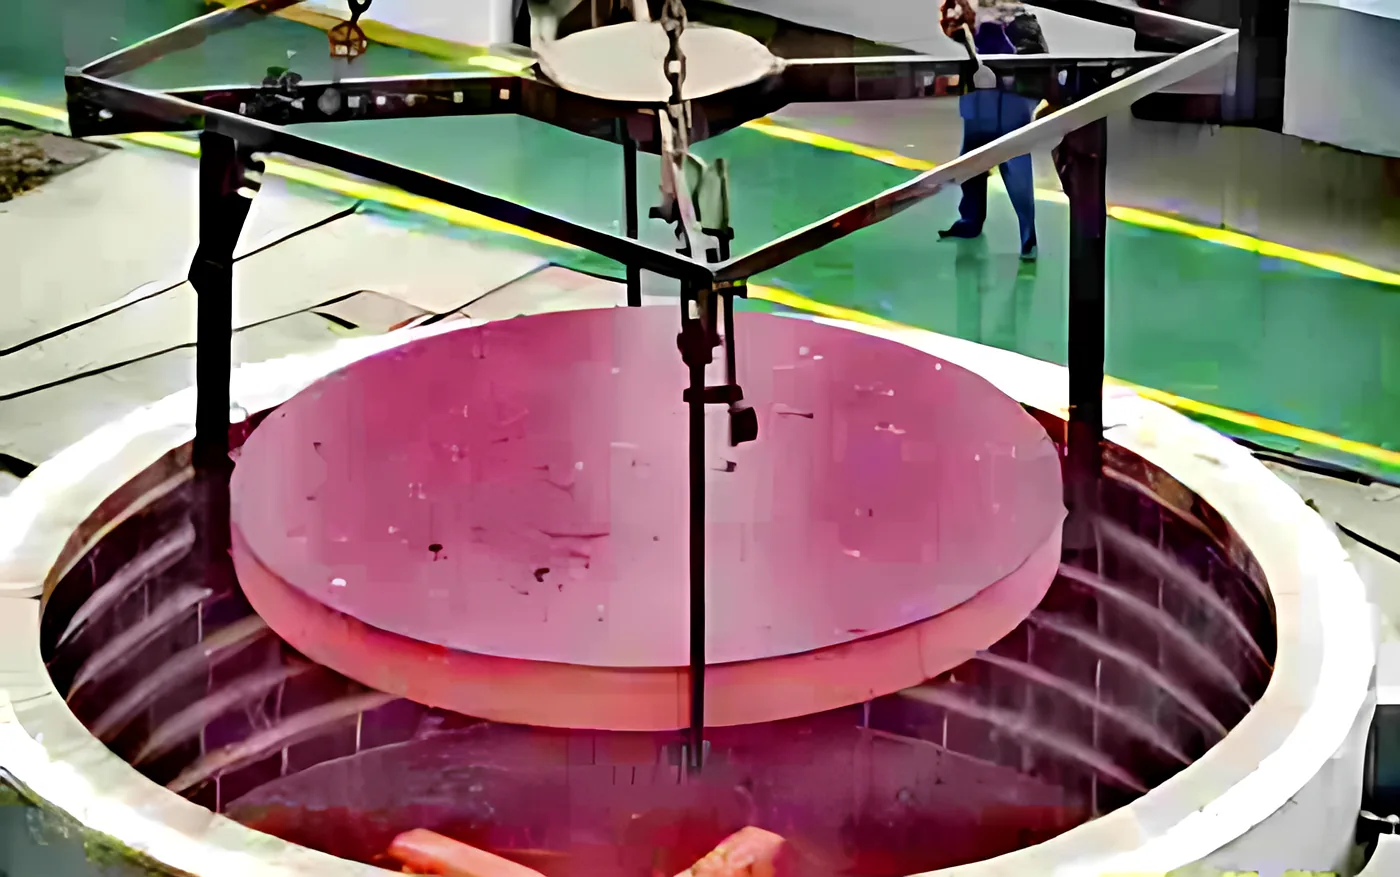
Large steel disc lifted from the quench tank during heat treatment

Heat treatment

Ten furnaces cover normalizing, quenching and tempering, annealing and solution treatment. A forklift quench line transfers parts into the tank in as little as 30 seconds for full through-hardening.

  • Induction hardening to 12 mm depth
  • Carburizing for gears and racks
  • Vacuum and pit furnaces
  • Forced air-cooling pit
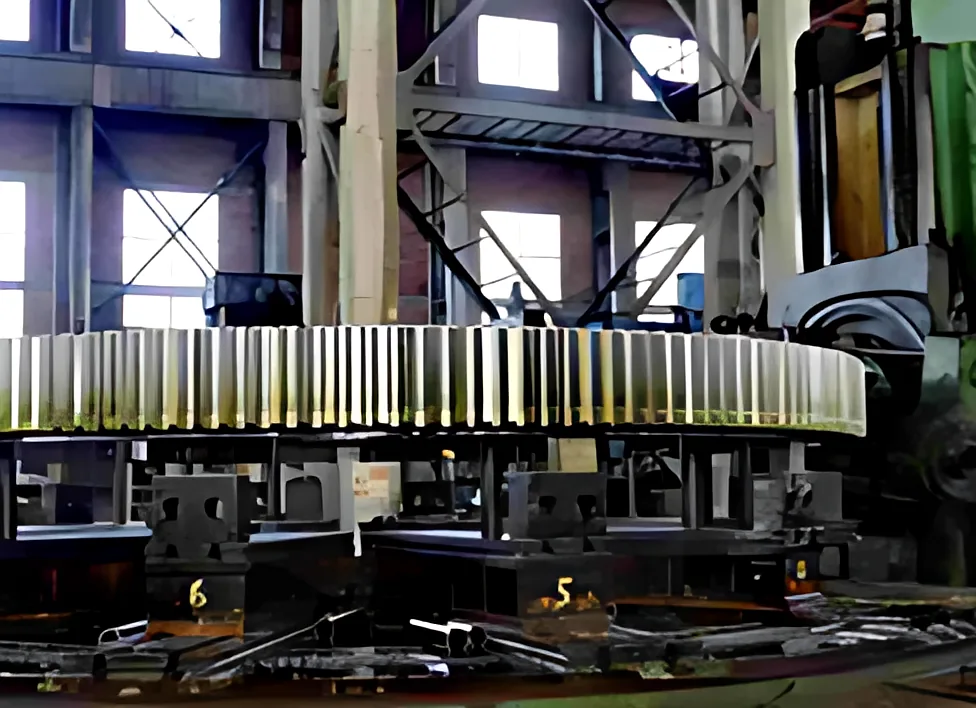
Gear hobbing machine cutting a large gear rim

Gear cutting

Hobbing, shaping and grinding of spur, helical and internal gears, splines and racks, from fine-pitch racks to coarse-module gear rims.

  • Gear racks, module 0.5–36
  • Internal ring gears and splines
  • DIN 5–DIN 10 precision
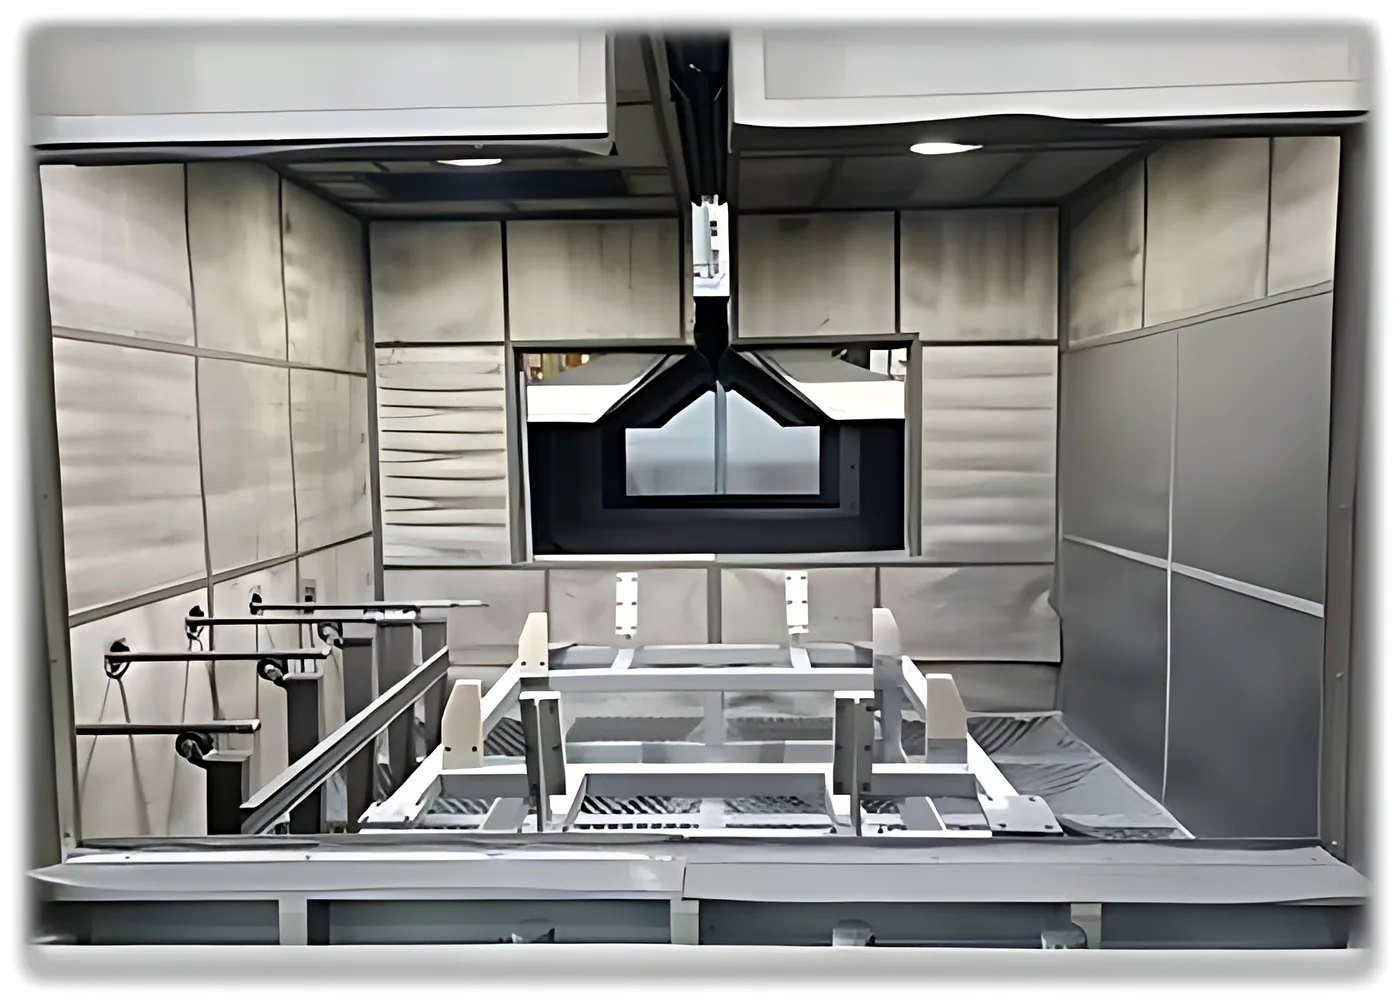
Automatic surface coating line for machined parts

Surface treatment & coating

An automatic coating line and paint booths apply primer and topcoat after machining. Plating and conversion coatings are selected to suit the service environment.

  • Zinc, nickel and hard chrome plating
  • Black oxide and phosphating
  • Epoxy and polyurethane paint systems
  • Laser cladding repair of shafts and flanges

At a glance

Capability summary

Machine capacities and typical results by process. Achievable tolerances depend on part size, material and geometry and are confirmed for every drawing.

Summary of Songyan Machinery machining and fabrication capabilities
ProcessMaximum capacityTypical accuracy / finishTypical parts
CNC turning & turn-millingØ3,200 mm class × 2,000 mm, 15 t0.01 mm · Ra 1.6–3.2 µmShafts, flanges, rings, hubs, bowls
CNC milling & horizontal boringX 5,000 × Y 3,200 × Z 2,500 mm, 50 t0.008–0.01 mmGearbox housings, frames, valve bodies
5-axis & gantry machiningX 4,230 × Y 2,650 mm class0.01 mmPlanet carriers, beds, complex housings
Cylindrical grindingØ630 × 4,000 mmIT5–IT6 · Ra 0.4–0.8 µmBearing journals, rolls, spindles
Laser cutting20 kW plate · 12 kW tubeClean narrow kerfBlanks, gussets, tubes, profiles
Robotic weldingØ3,650 mm positioner, 6 tVisual, MT, UT verifiedRotor shafts, frames, housings
Forming400 t × 3,200 mm press brake—Brackets, covers, channels
Heat treatment10 furnaces · induction to 12 mmHardness to drawingShafts, gears, racks, wear parts
Gear cuttingRacks module 0.5–36DIN 5–DIN 10Racks, spur, helical and ring gears

Capabilities FAQ

Questions about our processes

Still unsure whether we can make your part? Send the drawing and we will confirm within the quotation.

Send a drawing
Can Songyan Machinery handle a part that needs cutting, welding, machining and painting?

Yes. Cutting, forming, welding, stress relief, CNC machining, heat treatment, grinding, inspection, coating and export packing all take place in our own workshops in Jiangyin. You place one order and receive a finished, documented part.

Do you machine customer-supplied castings and forgings?

Yes. We regularly machine free-issue castings and forgings. Incoming parts are inspected and recorded on arrival, and we can add NDT, 3D scanning of as-cast surfaces and chemical verification before machining starts.

Are welded parts stress-relieved before machining?

Yes, when the design requires it. Weldments are stress-relieved thermally in a trolley tempering furnace or by vibratory stress relief before final machining, so bores and faces remain stable after machining.

What surface roughness can you achieve?

Typical results are Ra 1.6–3.2 µm for turned and milled surfaces and Ra 0.4–0.8 µm for ground surfaces. Finer finishes can be achieved on suitable geometry and are confirmed during drawing review.

Can you machine large parts on 5-axis equipment?

Yes. Our 5-axis gantry machining centers handle large housings and carriers in a single setup, and horizontal boring centers with rotary tables machine four faces of parts up to 50 t in one clamping.

Request a quote

Send your drawings. Get a price and lead time.

Email sales@symachiningparts.com or message us on WhatsApp at +86 189 1530 7612. All drawings are treated as confidential.